Best Ultrasonic Spray Systems for Every Precision Coating Need
2026-11-03
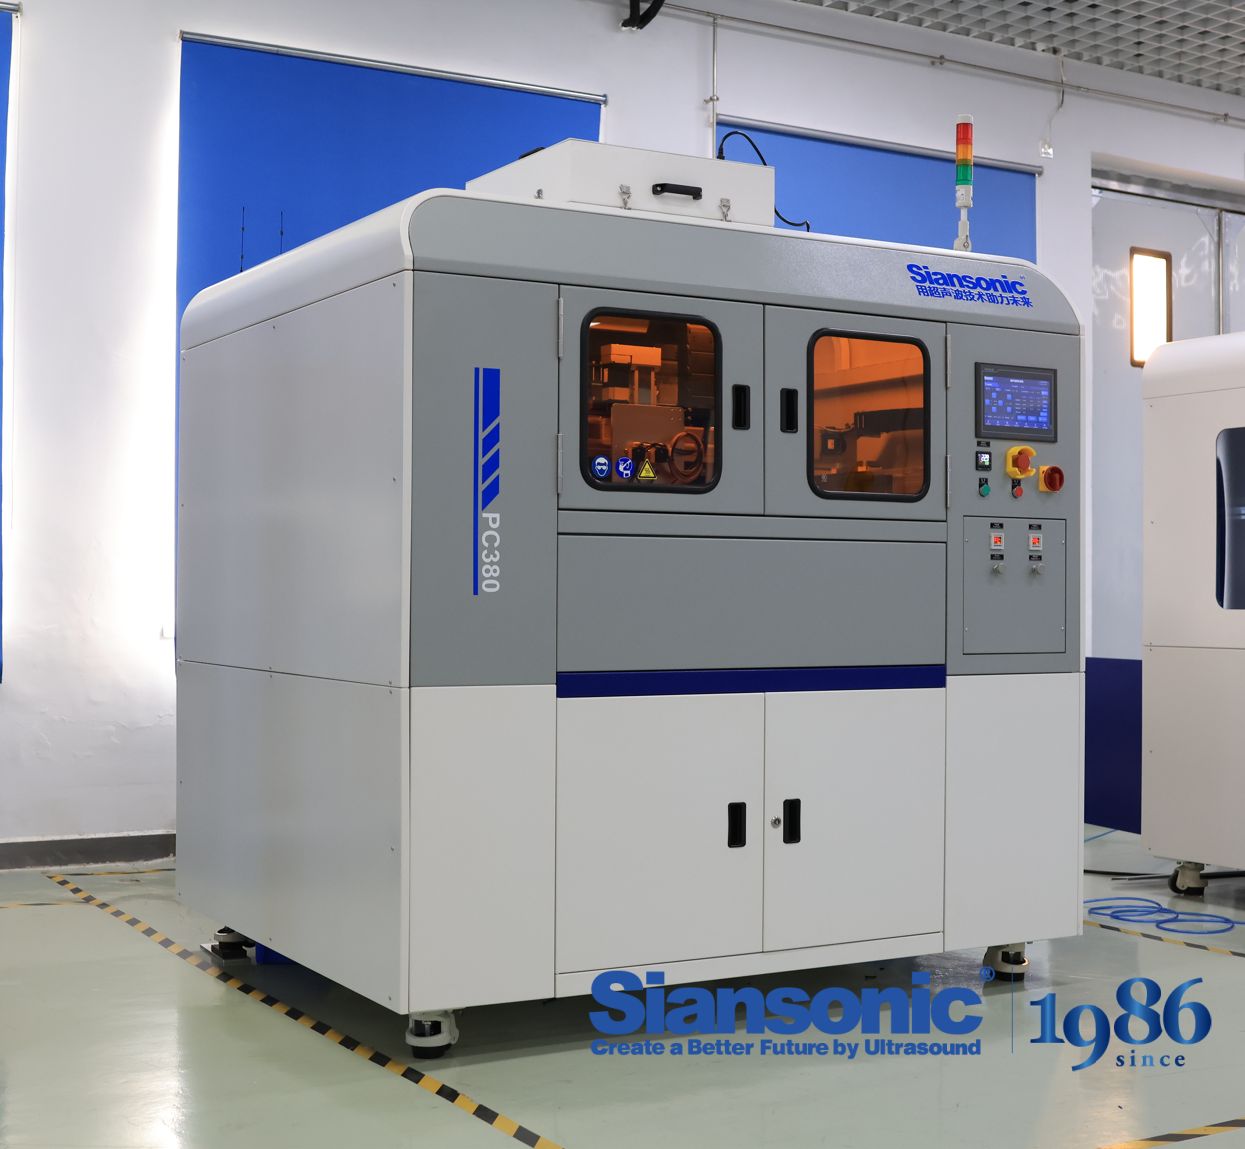
Precision coating demands more than just atomization—it requires control at the micron level. For engineers and researchers pushing the limits of thin-film uniformity, Siansonic's ultrasonic spray systems have become the quiet workhorse in labs and production lines alike. But with so many configurations available, how do you match the right system to your specific substrate, viscosity, and throughput? This guide cuts through the noise, comparing the top Siansonic models across real-world coating scenarios—from fuel cells to medical devices—so you can stop guessing and start coating with confidence.
Coating Uniformity That Holds Up Under a Microscope
A uniform coating looks flawless to the naked eye, but that impression rarely survives contact with a microscope. Even a few hundred nanometers of thickness variation can create visible streaks, pinholes, or light interference patterns at high magnification. Achieving true microscopic uniformity means controlling particle dispersion, solvent evaporation rate, and substrate wetting simultaneously. Any one of these factors drifting outside a narrow window will leave behind a signature defect that becomes obvious under 100x magnification.
The difference between a decent coating and an exceptional one shows up in how flat the dried film remains across a textured surface. On a brushed metal panel, for example, a well-engineered coating follows the micro-roughness without pooling in valleys or starving the peaks. This kind of conformal coverage requires careful rheology adjustment rather than simply adding more solids. When the film thickness profile stays within a tight tolerance across every square millimeter, the coated part not only looks better but also performs more predictably in real-world conditions.
When Overspray Is Not an Option
Some finishes demand a level of control that a wide spray pattern simply cannot deliver. When you're working with intricate trim, tight corners, or surfaces bordered by materials that must remain untouched, overspray becomes more than a nuisance—it becomes a liability. That's when you reach for a method that keeps every drop where it belongs.
Brushwork or rolling might feel slower, but they offer the precision that spraying forfeits the moment the trigger is pulled. Consider the edge of a painted cabinet door meeting stained wood, or a wall color stopping cleanly at a hand-painted mural. In these cases, the time spent masking and tenting could easily exceed the time saved by spraying. And if the masking fails, the cleanup costs more than the paint itself.
There's also the matter of material thickness. Some coatings—like high-build primers or specialized adhesives—are formulated to be applied in a controlled film, not atomized into the air. Trying to force them through a sprayer can clog tips, alter drying times, and compromise the final surface. When the job calls for deliberate placement rather than broad coverage, the choice is clear: put the sprayer down and pick up the tool that respects the boundaries in front of you.
The Quiet Efficiency of Piezoelectric Precision
A slab of quartz or a sliver of PZT ceramic will change shape by mere nanometers when voltage is applied—no spinning rotors, no clattering gears, just a lattice of atoms shifting in near silence. That direct conversion of electrical energy into mechanical strain is what gives piezoelectric devices their unique hold on precision. Unlike motor-driven stages that rely on bearings and lead screws, a piezo stack can hold a position with sub-atomic resolution while consuming almost no power at rest. The quiet here isn't just acoustic; it's the absence of friction, backlash, and wear that normally accumulate in moving systems.
In scanning probe microscopes and semiconductor lithography tools, this silent motion translates into images and patterns that would be impossible with conventional actuators. A piezoelectric tube flexes a few microns to trace the topography of a single molecule, then returns to center without ever overshooting. Medical micropumps dose insulin using bending discs that operate below the threshold of human hearing, while adaptive optics in telescopes realign mirrors thousands of times per second to cancel atmospheric shimmer. In each case, the efficiency is not measured in horsepower but in the ability to do extremely small, repeatable work without wasting energy as heat or sound.
Of course, piezoelectric materials have their quirks: hysteresis makes the displacement curve loop back on itself, and creep causes slow drift after a voltage step. Engineers counter these with closed-loop feedback and charge-controlled amplifiers, trading a little complexity for the sake of nanometer certainty. That compromise is worth it because, in the realm of the infinitesimally small, a mechanism that moves without noise, backlash, or wasted motion becomes the quiet workhorse behind modern instrumentation.
From Lab Bench to Production Line Without Relearning
Most teams accept the usual drift: a model or script that works perfectly in a notebook starts failing the moment it hits shared infrastructure. The reason is rarely the algorithm, but the environment. This approach removes that gap by keeping the exact same runtime, dependencies, and configuration from the first experiment to the final deployable artifact. You do not adapt your work to a new platform; the platform adapts to the way you already work.
Instead of introducing a separate production stack that requires its own set of skills, the tooling stays identical across stages. The commands you use to run a local training job are the same ones that trigger a distributed run. Logging, data access, and model packaging work the same way whether you are on a laptop or a cluster. That means no translation layer, no hand-off documents, and no late-night debugging sessions caused by mismatched versions.
The practical result is that researchers and engineers stop thinking of production as a separate discipline. A pipeline that works at small scale can be pointed at larger resources with a single parameter change, not a rewrite. Teams ship faster because the work they already validated is the work that actually runs.
Thin Films, Tight Tolerances, No Guesswork
A thin-film run either lands inside the tolerance window or it doesn't. We monitor thickness in real time with quartz crystal microbalances and optical reflection data, so the deposition shuts off at the exact target rather than at an estimated time. That removes the most common source of error: drift between calibration and actual chamber conditions.
Tight tolerances don't stop at one layer. In a stack of 30 or 40 films, small rate variations at the substrate edge compound fast. We map the deposition profile and adjust power or gas flow per zone, then verify finished parts with spectrophotometry and profilometry. The measured curve matches the design without rework loops.
What that means on the floor is no guesswork. The operator loads a recipe, the tool pulls calibration data for the material set, and the first run behaves like the tenth. When parameters shift, the system flags the drift instead of letting it hide until final test.
Built for the Materials That Fight Back
Most tooling is designed for materials that give way easily. But hardened steel, titanium alloys, and wear plate push back—they dull edges, generate intense heat, and vibrate through the frame. This system was built from the ground up to absorb that punishment instead of fighting it.
The spindle and guideways are oversized and preloaded, so there's no chatter when the cutter bites into a tough workpiece. Instead of relying on a single hard coating, the contact surfaces use a staged approach: a tough underlayer for impact, a hard outer layer for abrasion, and a micro-texture that breaks up chip adhesion. It means the tool keeps its geometry longer when working with materials that would wreck standard equipment in an afternoon.
In practice, that translates to fewer passes on hardened dies, cleaner threads in stainless, and less time swapping out inserts. Operators can push feed rates closer to the material's actual limit, because the machine isn't the weak link—the workpiece is. That's a different kind of confidence on the shop floor.
FAQ
Ultrasonic nozzles use high-frequency vibration to create a soft, low-velocity mist. That reduces overspray and bounce-back, so more coating stays on the part and you can handle fragile surfaces without blowing them around.
Medical device manufacturing, electronics, fuel cells, and glass coating are common. Anywhere you need a thin, uniform layer on a complex surface, ultrasonic systems tend to outperform traditional methods.
Start with your coating viscosity, desired wet film thickness, and part geometry. Low-viscosity fluids work well with standard ultrasonic nozzles, while higher-viscosity or particle-laden fluids may require a different nozzle design or a heated delivery system.
Yes, many systems are built for that. You can get precise flow control down to microliters per minute, which is ideal for prototyping, lab testing, or producing small batches without wasting expensive coating materials.
Regular cleaning with the appropriate solvent is important, especially if you're spraying polymers or nanoparticle suspensions. Avoid running the nozzle dry for long periods, and check the tip for buildup. Most issues come from clogging rather than mechanical failure.
They can be, but you often need to pair the nozzle with a multi-axis motion system or rotate the part. The soft mist follows contours better than a high-pressure jet, but line-of-sight still matters, so complex recesses may need special fixturing.
Typically you can achieve variations under ±5% across a flat surface, and even better with optimized parameters. The key is consistent flow rate, stable nozzle-to-substrate distance, and proper atomization power.
They work with both. Water-based coatings sometimes need slightly different power settings because of surface tension, but ultrasonic nozzles handle aqueous solutions, suspensions, and solvent-based formulations equally well.
Conclusion
Precision coating demands more than a fine mist—it requires a system that thinks in microns and delivers the same pattern at hour one as at hour one thousand. Ultrasonic spray systems built for exacting work achieve exactly that, with coating uniformity that stands up under a microscope. The gentle, low-velocity spray produced by piezoelectric transducers not only preserves the integrity of delicate substrates but also eliminates overspray when every droplet counts. There is no pulsing air blast to disturb the film, no ragged edge to trim later. Instead, the quiet efficiency of high-frequency oscillation turns even the most temperamental materials—suspensions, nanoparticles, polymers that fight back—into a controlled, repeatable layer.
What makes these systems truly practical is how seamlessly they move from the lab bench to the production line without forcing operators to relearn a process. Thin films with tight tolerances no longer rely on guesswork; the nozzle geometry, flow rate, and standoff distance can be locked in, so the same recipe yields the same result across shifts and scales. Whether you are coating a medical stent with a drug-eluting film or depositing a conductive layer on a flexible sensor, the combination of low overspray, uniform deposition, and material versatility removes the usual trade-offs. You get the precision of a laboratory tool with the throughput of a proven manufacturing asset—no guesswork, no drift, just a reliable coat every time.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/