OEM Anti-static Floor Systems Essential Guide for Industrial Buyers
2026-11-16
Choosing the right anti-static flooring for an industrial facility is a decision that directly impacts equipment safety and operational uptime—yet many buyers still rely on generic specifications that fail under real-world conditions. This guide cuts through the noise for OEM procurement teams, offering practical criteria on material conductivity, load ratings, and long-term maintenance. As a manufacturer with decades of precision flooring expertise, Huahong brings field-tested insights that help you avoid costly mismatches between spec sheets and actual performance.
Where Static Electricity Threatens Sensitive Equipment Floors
Static discharge rarely announces itself. In semiconductor fabrication areas, wafer handling stations, and microelectronics assembly benches, a voltage far below the threshold of human perception can erase memory cells or punch through oxide layers. These rooms often combine low humidity, fast-moving automated equipment, and insulating materials, which turns ordinary movement into a constant source of charge buildup.
Data centers and server rooms face a quieter version of the same problem. Racks filled with tightly packed circuit boards leave little margin for error. A technician sliding a chassis across a carpeted office floor or even pulling off a strip of vinyl tape can generate enough potential to degrade a network interface card. Over time, repeated small discharges cause intermittent failures that are difficult to trace.
Some environments carry an additional risk beyond component damage. Chemical mixing rooms, solvent storage areas, and printing operations where flammable vapors linger can be ignited by a single spark. Pharmaceutical cleanrooms and optical labs also suffer from static because charged surfaces attract dust and fibers, compromising sterility or coating quality. In these spaces, controlling floor conductivity is not just about uptime; it is part of the safety and quality system.
Conductive Versus Dissipative: Matching Floor Properties to Your Workflow
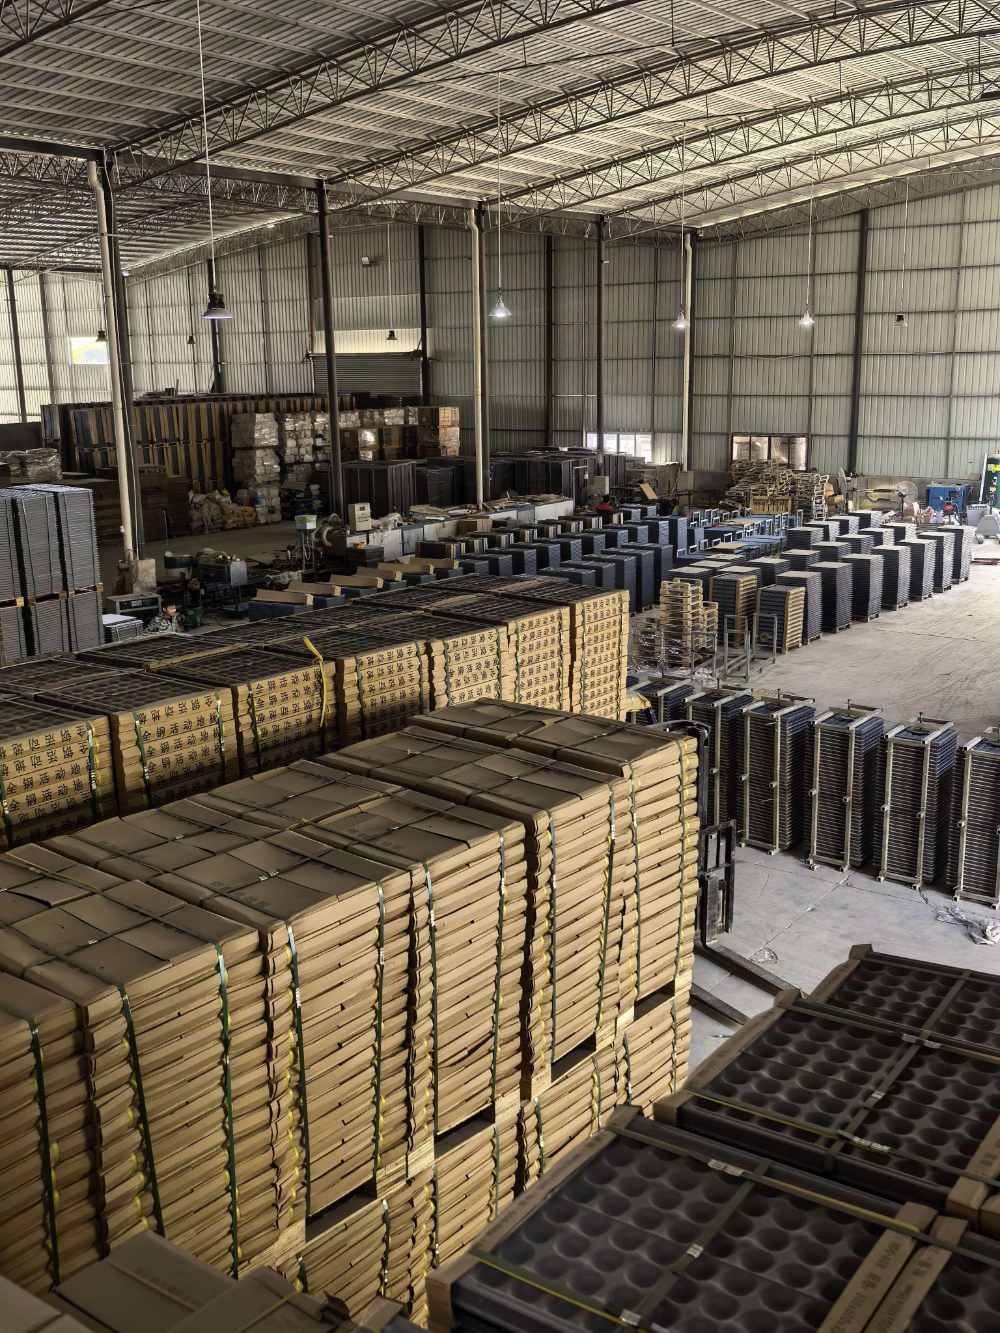
Conductive floors typically fall below 1.0 x 10^6 ohms, allowing static charges to bleed off almost instantly. That speed is valuable in spaces where even a brief voltage drop can ruin sensitive electronics or ignite airborne solvents. But rapid discharge also means any worker who accidentally contacts a live circuit may feel a sharper shock, since the floor does little to slow the current. If your process involves both electrical tools and static-sensitive parts, that trade-off may not be worth the faster drain.
Dissipative flooring sits between 1.0 x 10^6 and 1.0 x 10^9 ohms, deliberately slowing the flow of static to a safer rate. This middle ground works well in mixed workflow areas such as repair benches, packaging lines, and labs where people regularly handle powered equipment. The floor still protects nearby components from static buildup, but it won't behave like a metal plate if a tool faults. In short, choose conductive when the workflow prioritizes maximum static removal above all else; choose dissipative when your staff and equipment share the same floor and electrical safety is equally important.
Actual performance depends heavily on footwear, humidity, and maintenance. A dissipative floor paired with ordinary insulated soles may not provide a reliable path to ground, no matter what the resistance rating says. Likewise, heavy wax finishes or dust layers can push real-world readings outside the intended range. Rather than chasing a lower ohm number, audit how static is generated in each work zone, how often people move between tasks, and what failure looks like if a discharge occurs. That context will tell you whether a fast or a controlled bleed-off better matches your workflow.
Installation Errors That Undermine Anti-static Floor Performance
One of the first places an installation goes wrong is the grounding grid. Copper strips get laid in a hurry, overlaps are too short, or a crew simply forgets to bond the grid to the building's earth point. The floor looks fine from above, but a simple resistance test across two tiles can show hundreds of kilo-ohms instead of the required range. That gap is where static builds up and eventually arcs through a component.
Uneven pedestals are another silent killer. If the subfloor has high spots or the pedestal heads are not levelled one by one, the finished surface flexes underfoot. Over time that movement works the grounding clips loose and cracks the conductive coating along the tile edges. What starts as a minor wobble becomes a dead zone where static charge has no path to ground.
Then there is the adhesive. Swapping the specified conductive adhesive for a cheaper general-purpose glue saves a few minutes but turns each joint into an insulator. The same applies to cutting tiles without resealing the edges. Raw cuts expose the inner core, which is often non-conductive, so the perimeter of every cut tile stops passing current. These small shortcuts repeat across a whole floor until the protection is effectively patchwork.
Daily Care Practices That Preserve Static Dissipation
Most static-dissipative surfaces fail slowly, not suddenly. A weekly wipe-down with a diluted antistatic cleaner keeps the conductive pathways from getting choked by dust, oil, or hand cream residue. Skip the furniture polish and floor wax—those leave an insulating film that can quietly undo the material's ability to bleed off charge. If the surface starts to feel tacky or shows a dull haze, that's usually the first sign the maintenance routine needs adjusting.
Footwear and contact points matter just as much as the surface itself. Check that heel straps and grounding cords aren't frayed, kinked, or tucked under equipment where they get stepped on. Even a well-maintained bench mat won't help much if the operator's shoes have built up a layer of insulative grime. A quick daily visual pass—looking for loose snaps, broken wires, or curled edges that trip people—catches most problems before they turn into intermittent ESD events.
Humidity control often gets overlooked because it's invisible. Keeping relative humidity in the 30–60% range makes it easier for surfaces to shed static, but over-relying on humidity alone can mask a failing dissipative layer. Rotate your verification meter across different spots, not just the same convenient corner, and log the readings. Trends matter more than single numbers; a steady downward drift in resistance usually tells you it's time to deep-clean or replace the material before a sensitive component pays the price.
Hidden Costs in Anti-static Floor System Ownership
When budgeting for an anti-static floor system, most facility managers focus on the initial purchase and installation price. But the real financial picture often emerges months or years later, in the form of expenses that were never listed on the original quote. These hidden costs can quietly erode the return on investment and catch even experienced buyers off guard.
One of the most overlooked expenses is the ongoing need for specialized cleaning and maintenance. Standard floor cleaners can leave residues that compromise conductivity, so you'll need approved anti-static solutions and microfiber mops—often at a premium. Over time, worn or damaged tiles must be replaced individually, and if the grounding system degrades due to moisture or subfloor shifts, an electrician may be needed to retest and repair the entire network. These routine upkeep tasks add up far beyond what a simple sweep might suggest.
Another hidden cost comes from operational disruptions and premature replacement. If a section of flooring fails and isn't caught early, static discharge can damage sensitive electronics, leading to expensive equipment repairs or data loss. In high-traffic areas, the wear layer may break down faster than expected, forcing partial or full replacement years before the warranty expires. And don't forget the cost of downtime: tearing up a floor in an active cleanroom or server room means halting operations, which can dwarf the price of the flooring itself.
Questions to Ask Before Signing with an OEM Floor Supplier
Before you commit to any OEM floor supplier, dig into their material sourcing and quality control process. Ask where the raw wood or laminate comes from, whether they have third-party testing reports for durability and formaldehyde emissions, and how they handle batch consistency. A supplier who can't clearly explain their QC steps or hesitates to share test data is likely cutting corners that will show up as warping, fading, or uneven finishes after installation.
Next, clarify the full scope of customization and lead times. Will they produce custom colors, plank sizes, or surface textures, and what are the minimum order quantities for each option? Request a sample run before full production, and pin down exact timelines for sampling, manufacturing, and shipping. Many delays happen because buyers assume standard lead times apply to custom orders—don't let that catch you off guard.
Finally, understand the warranty and after-sales support in writing. What happens if a percentage of the order arrives damaged or defective? Who covers the cost of replacement boards, and how quickly can they ship them? Also ask about long-term availability: will the same product be available for touch-ups or expansions two years from now? A supplier that goes silent after the invoice is paid will leave you holding the bag on any future project needs.
FAQ
A genuine OEM solution is engineered with your production workflow, not just a material with a conductive additive. It involves matching tile or coating chemistry to your specific humidity swings, traffic patterns, and equipment grounding requirements. You get full documentation, surface resistivity tests per ESD S7.1, not just a sales sheet, and the ability to have the system branded or re-specified for your downstream clients without re-engineering.
If you move sensitive electronics, handle volatile powders, or operate in a room where a 100-volt body charge can kill a component, you need verified static decay, not just paint. An OEM system lets you tailor the resistance range, usually 10^6 to 10^9 ohms, and choose your finish, thickness, and edge details. Standard epoxy rarely ships with a full ESD sign-off for your audit trail.
No. They appear in cleanrooms, munitions handling, pharmaceutical powder rooms, server halls, and even aerospace assembly. The OEM angle matters where you need the floor to be part of a larger certified environment, think modular tiles that integrate with grounding busbars you already spec. If the floor is just a standalone purchase, you lose the custom engineering link.
Ask for third-party test data from your actual substrate, not a lab coupon. Confirm the warranty covers both the material and the static-dissipative performance over time. Look at how the OEM handles seams, cove bases, and penetrations, those are where static leaks happen. And insist on a mock-up section before full installation.
It depends on the subfloor's condition and the system design. Some OEM systems use interlocking conductive rubber tiles that sit over raised panels if the panels are clean and grounded. Others require stripping to bare concrete for a conductive primer. The right OEM partner will map the resistance from the top surface to your building's earth ground first, then decide.
You pay for the engineering behind material selection, grounding layout, and post-install verification. Off-the-shelf tiles may meet a spec in isolation but fail when your ambient humidity drops or your equipment shifts. An OEM solution is often cheaper than a failed audit or a batch of dead PCBs.
With proper maintenance, a high-quality OEM system can last 10-15 years or more. The anti-static properties are built into the material, not just a surface coating, so they don't wear off like a wax. You will still need periodic resistance checks and cleaning with ESD-safe solutions to keep the surface conductive and clean.
Daily or weekly dry mopping with a carbon-impregnated mop, quarterly resistance testing, and immediate repair of any gouges or chemical spills. Avoid waxes and insulating finishes, they create an insulative layer that breaks the static path. The OEM should supply a maintenance manual tied to your specific floor chemistry.
Conclusion
In electronics assembly, server rooms, and clean manufacturing, even a minor electrostatic discharge can scramble data or degrade microcircuits long before failure appears. This guide walks through what actually matters when sourcing OEM anti-static flooring. Start by mapping the workspace: areas with highly sensitive components often need conductive flooring, while dissipative surfaces suit workflows where controlled charge bleed is enough. But the wrong choice is only part of the risk. Installation mistakes, such as improper grounding points, stretched or torn copper strips, or adhesive gaps under panels, quietly defeat the system's performance. A floor can look flawless and still fail continuity tests if the grid is not bonded correctly. Smart buyers ask to see post-installation resistance measurements, not just product data sheets.
Long-term costs hide in maintenance habits and supplier support. Daily cleaning with ordinary detergents leaves insulating films that block static dissipation, so the care routine must match the floor chemistry. Also factor in replacement tiles, grounding audits, and training for custodial staff; these often outweigh the initial purchase price. Before signing with an OEM supplier, ask about their testing protocol, warranty terms tied to measured resistance, availability of spare parts, and how they handle drift over years. A reputable partner will discuss failure modes openly and provide clear thresholds for when sections need repair. Compare not only square-meter pricing but also lifecycle expense, including interruption losses if flooring degrades unnoticed. The right floor is not a one-time purchase; it is a system that demands verification, proper care, and a supplier willing to stand behind measurable performance.
Contact Us
Contact Person: Hai-Bo Xiao
Email: [email protected]
Tel/WhatsApp: 8618898711810
Website: https://www.huahongfloor.com