Optical Comparator Manufacturer Tips for Choosing the Right Inspection System
2026-09-23
Selecting an optical comparator isn’t just about magnification—it’s about matching the system to your unique inspection challenges, from tight tolerances to high-volume throughput. With so many manufacturers claiming superiority, making the right choice can feel like guesswork. That’s why JATEN, a trusted optical comparator manufacturer, breaks down the key factors you should weigh before investing, ensuring your next inspection system delivers precision without hidden compromises.
Verify Stage Travel and Workpiece Clearance Before You Commit
Before you trust the CAM screen, grab the handwheel and take the spindle through every extreme corner of the program. Watch the longest tool you plan to use, not just the one that is currently loaded. Clamps, vise jaws, tailstocks, and rotary fixtures have a way of ending up closer to a rapid move than the model suggests. If the setup sheet says clearance is fine at Z-4.2 but the actual tool holder tapers inward, you may still clip the top of a toe clamp during a lateral move.
A dry run with the part out of the fixture is not optional when the material cost is high. Feed hold through the first pass and keep one finger near the spindle override. Mark the physical locations of every bolt and support, then walk around the machine to compare them against your safe zones. If an axis needs to travel within a quarter inch of an obstruction, slow that section down or shift the workpiece rather than hoping the postprocessor calculated the exact same clearance as your eyes.
Only after you measure the actual distance between the tool nose and the nearest hard point at the worst-case positions should you hit cycle start with stock in place. Write those measured gaps directly on the setup sheet, and check them again after the first tool change. Ten minutes spent here is cheaper than replacing a spindle or explaining a gouged tombstone to the shop floor.
Look Past Screen Size to Actual Edge Detection and Overlay Quality
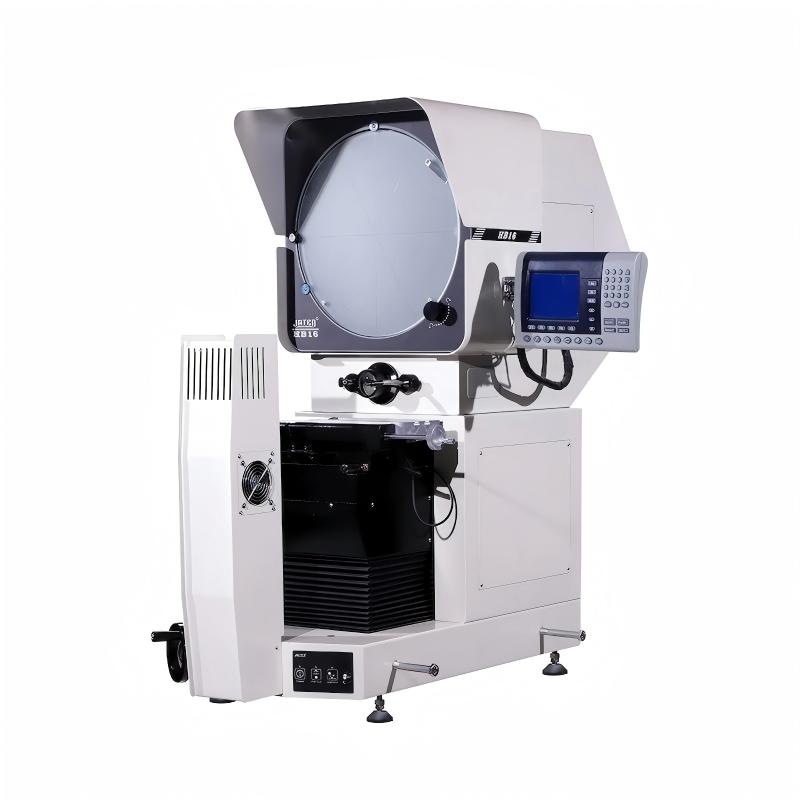
Screen dimensions tell you little about how a panel actually meets its frame. Two displays with identical diagonal measurements can behave very differently at the borders. The real difference shows up in edge detection: how precisely the active area ends, whether the bezel masks it cleanly, and whether the touch layer remains accurate near the perimeter.
Overlay quality is another layer that size specs miss. A slightly larger screen with a poorly bonded cover glass can look washed out or distorted compared to a smaller screen with a well-matched overlay. Haze, internal reflections, and uneven lamination become obvious when you view off-axis or under bright light. These flaws never appear in a size chart.
If you are comparing devices or panel samples, ignore the marketing diagonal for a moment and run your finger or a test pattern near the edges. Look for color shifts, backlight bleed, and inconsistent touch response. Check how the overlay sits against the frame and whether it creates a visible border or shadow. Those small details predict daily comfort far more than an extra tenth of an inch.
Question Subpixel Accuracy Claims with Repeatability Tests
Subpixel accuracy claims often sound impressive in marketing materials, but without repeatability tests they carry little weight. A single measurement or a carefully staged demo can easily hit a subpixel target due to favorable noise, lighting, or target geometry. The real question is whether the system can hit that same level again and again under identical conditions. Repeatability tests expose the underlying stability of the algorithm and hardware. If a vision system drifts by a few hundredths of a pixel between consecutive runs, then calling it "subpixel accurate" is misleading. True subpixel performance means the spread of repeated measurements stays within a fraction of a pixel, not just that one lucky result landed there.
To fairly evaluate repeatability, the test needs to control environmental factors that can silently inflate variance. Temperature shifts, slight vibrations, or changing illumination can push the measured position around by more than the claimed subpixel margin. The target itself also matters: a high-contrast edge with strong gradient gives the interpolation algorithm an easy job, while a low-contrast or textured surface might cause the reported position to jump unpredictably. A meaningful repeatability study should report the standard deviation over dozens or hundreds of trials, not just the mean error. If an accuracy claim comes with only a handful of data points or no mention of environmental controls, it is fair to question whether the subpixel precision holds up outside the demo room.
Compare Illumination Sources, Lenses, and Mirror Coatings Side by Side
Placing an LED, a halogen bulb, and a mercury arc lamp next to each other quickly shows why modern microscopy favors the first. The LED reaches full intensity without warm-up and holds its color temperature across output levels, while halogen drifts warmer as you dim it and the arc lamp needs a bulky external power supply. In side-by-side use, the LED is also the only one that can be switched on and off repeatedly without shortening its usable life.
For objectives, an achromat, a plan achromat, and an apochromat differ most at the edges. The achromat is sharp in the center but shows noticeable color fringing and field curvature toward the periphery. A plan achromat flattens that field so a sample stays in focus across the frame, and an apochromat goes further by bringing red, green, and blue to the same focal point—something you notice immediately when photographing fine detail in brightfield.
Aluminum, silver, and dielectric mirror coatings each trade reflectivity for durability. Aluminum is forgiving in humid air but loses a little light in the visible range. Silver reflects more across visible wavelengths but tarnishes unless sealed, while dielectric coatings can be tuned for a narrow band and are more scratch-resistant, though they cost more. When all three are checked with a broadband light source, the silver mirror often looks brightest, but the dielectric mirror holds that brightness longer in a working lab.
Ensure the Comparator Exports Data into Your Existing Workflow
A comparator only becomes useful when its results flow naturally into the tools your team already trusts. If you have to copy columns by hand or re-enter values into a project tracker, the comparison step turns into busywork. Before committing to any tool, check whether it can send output directly to your spreadsheets, issue tracker, or internal dashboard.
Look beyond a generic “export CSV” button. The best options let you map comparator fields to your existing column names, include only the rows that changed, and schedule recurring exports or call an API endpoint. That kind of control means the data arrives in a shape your current setup can consume without manual cleanup.
Don’t just read the feature list—run a small test with a real dataset from last month. Export the results, import them into your normal workflow, and see if anything breaks. If the process needs extra formatting scripts or a middleman tool, the integration is probably not as smooth as the product page suggests.
Check the Manufacturer's Calibration Support and Spare Parts Availability
Not every instrument maker stands behind their equipment once it leaves the warehouse. Some will ship you a device and then vanish when you ask about recalibration intervals or where to find a replacement sensor. Before committing to a purchase, dig into how the manufacturer handles calibration support. Do they offer in-house calibration services, or do they point you toward third-party labs? What are the typical turnaround times, and do they provide loaner units while yours is being serviced? A company that maintains a dedicated calibration department and publishes clear procedures is generally a safer bet than one that treats calibration as an afterthought.
Spare parts availability is another area where short-term savings can turn into long-term headaches. A low upfront price means little if a simple O-ring or diaphragm fails and you discover the part is no longer manufactured, or that the only source is an overseas distributor with a six-week lead time. Ask for a list of common wear items and their expected lifespan. Check whether the manufacturer keeps parts in stock for older models and how many years after discontinuation they commit to supplying spares. The best companies will have a track record of supporting instruments a decade or more after they stop selling them.
Also look at the manufacturer's public documentation. Do they publish calibration manuals, troubleshooting guides, and exploded-view diagrams with part numbers? Is there a local distributor or service center you can call without navigating a maze of international support tickets? A quick way to test this is to send a pre-sales question about calibration or spare parts and see what kind of response you get. If the answer is vague, slow, or pushes you to buy a new unit instead of repairing the old one, that tells you a lot about the support you will receive down the road.
FAQ
Look beyond the headline magnification. Check how the stage handles heavy or awkward parts, whether the surface illumination is even at the edges, and if the lens mounting allows quick swaps without recalibration. These details affect daily usability more than the spec sheet suggests.
Vertical designs suit flat parts like stamps or gaskets and save bench space, while horizontal units handle turned or cylindrical components better because gravity helps seat them against the fixture. Think about the shape you inspect most often, not just the largest part.
They can reduce operator fatigue if you need to document measurements or share images across shifts. However, a poorly integrated camera that adds lag or forces you to switch between screens will slow you down. Ask for a live demo with your own sample parts before deciding.
Edge detection is where repeatability is won or lost. Advanced systems automatically pick up faint or low-contrast edges, while basic ones may require manual tracing. If your parts have polished surfaces or complex contours, invest in a comparator with robust automatic edge sensing.
Software often determines whether your team will actually use the system. Look for simple CAD import, one-click part programming, and clear reporting. Clunky menus or limited file formats will create a bottleneck even if the optics are excellent.
Request specific response times, whether calibration can be done on-site, and if loaner units are available during service. Also ask for a sample calibration certificate to see how traceable their process is. A manufacturer that hesitates on these details may cost you downtime later.
Usually not well. A stage that travels far enough for large parts may sacrifice fine resolution for small details. If your mix includes both extremes, consider a modular system or a secondary lens/stage configuration rather than forcing one setup to do everything.
Conclusion
Before you settle on an optical comparator, spend real time at the machine. Verify that the stage travel matches your largest part dimensions and that there is enough clearance for odd-shaped workpieces—this is often where a promising system falls short. Do not let a big display fool you; ask to see actual edge detection and overlay quality under your own lighting conditions, because screen size has little to do with measurement accuracy. Also, if a supplier boasts subpixel accuracy, push for repeatability tests on a known artifact, not a polished demo. Run the same measurement ten times and watch the spread.
Side-by-side comparisons of illumination sources, lens choices, and mirror coatings matter more than catalog specs. A bright LED ring may wash out edges that a collimated green light resolves cleanly. Beyond optics, confirm that the comparator can export data directly into your existing inspection workflow—CSV, DXF, or a live SPC link—without forcing a separate software island. Finally, ask the manufacturer how they handle calibration support and spare parts. A local service partner and a shelf of critical components can mean the difference between a day of downtime and a month. These practical checks separate a tool you will rely on from one you will regret.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/