Profile Projector Machine Selection: A Practical Guide to Choosing the Right Model
2026-09-27
Choosing a profile projector isn't just about magnification and screen size — it's about matching optical clarity, stage travel, and measurement software to what your shop actually inspects every day. In this guide, we break down the factors that separate a machine you'll outgrow from one that earns its place on your bench. We'll also look at how JATEN addresses these practical selection criteria across its range.
Start With the Dimensions You Can’t Compromise On
Ignore the pretty finishes for a moment. The real constraint is a doorway that measures 29 inches across or a radiator that juts out exactly where you'd planned a built-in shelf. Write down every measurement that cannot move—clearances, load-bearing walls, appliance widths—and let those numbers drive the layout. This keeps you from designing a beautiful piece that physically won’t fit through the front door.
Once the non-negotiables are on paper, you’ll notice they start to shape the project in useful ways. A hallway height restriction might force a lower profile, which then becomes a design feature rather than an afterthought. Instead of fighting the space, you work with the few measurements that refuse to budge, and that discipline removes most of the guesswork from the rest of the process.
People often try to soften a hard dimension or shave an inch here and there, but that’s where projects stall. Accept the fixed numbers early and you free up mental energy for choices that actually matter—materials, proportions, finishes. The result feels intentional because it was built from the inside out, not squeezed into a space that was never going to cooperate.
Look Past Magnification Claims to Real Optical Clarity
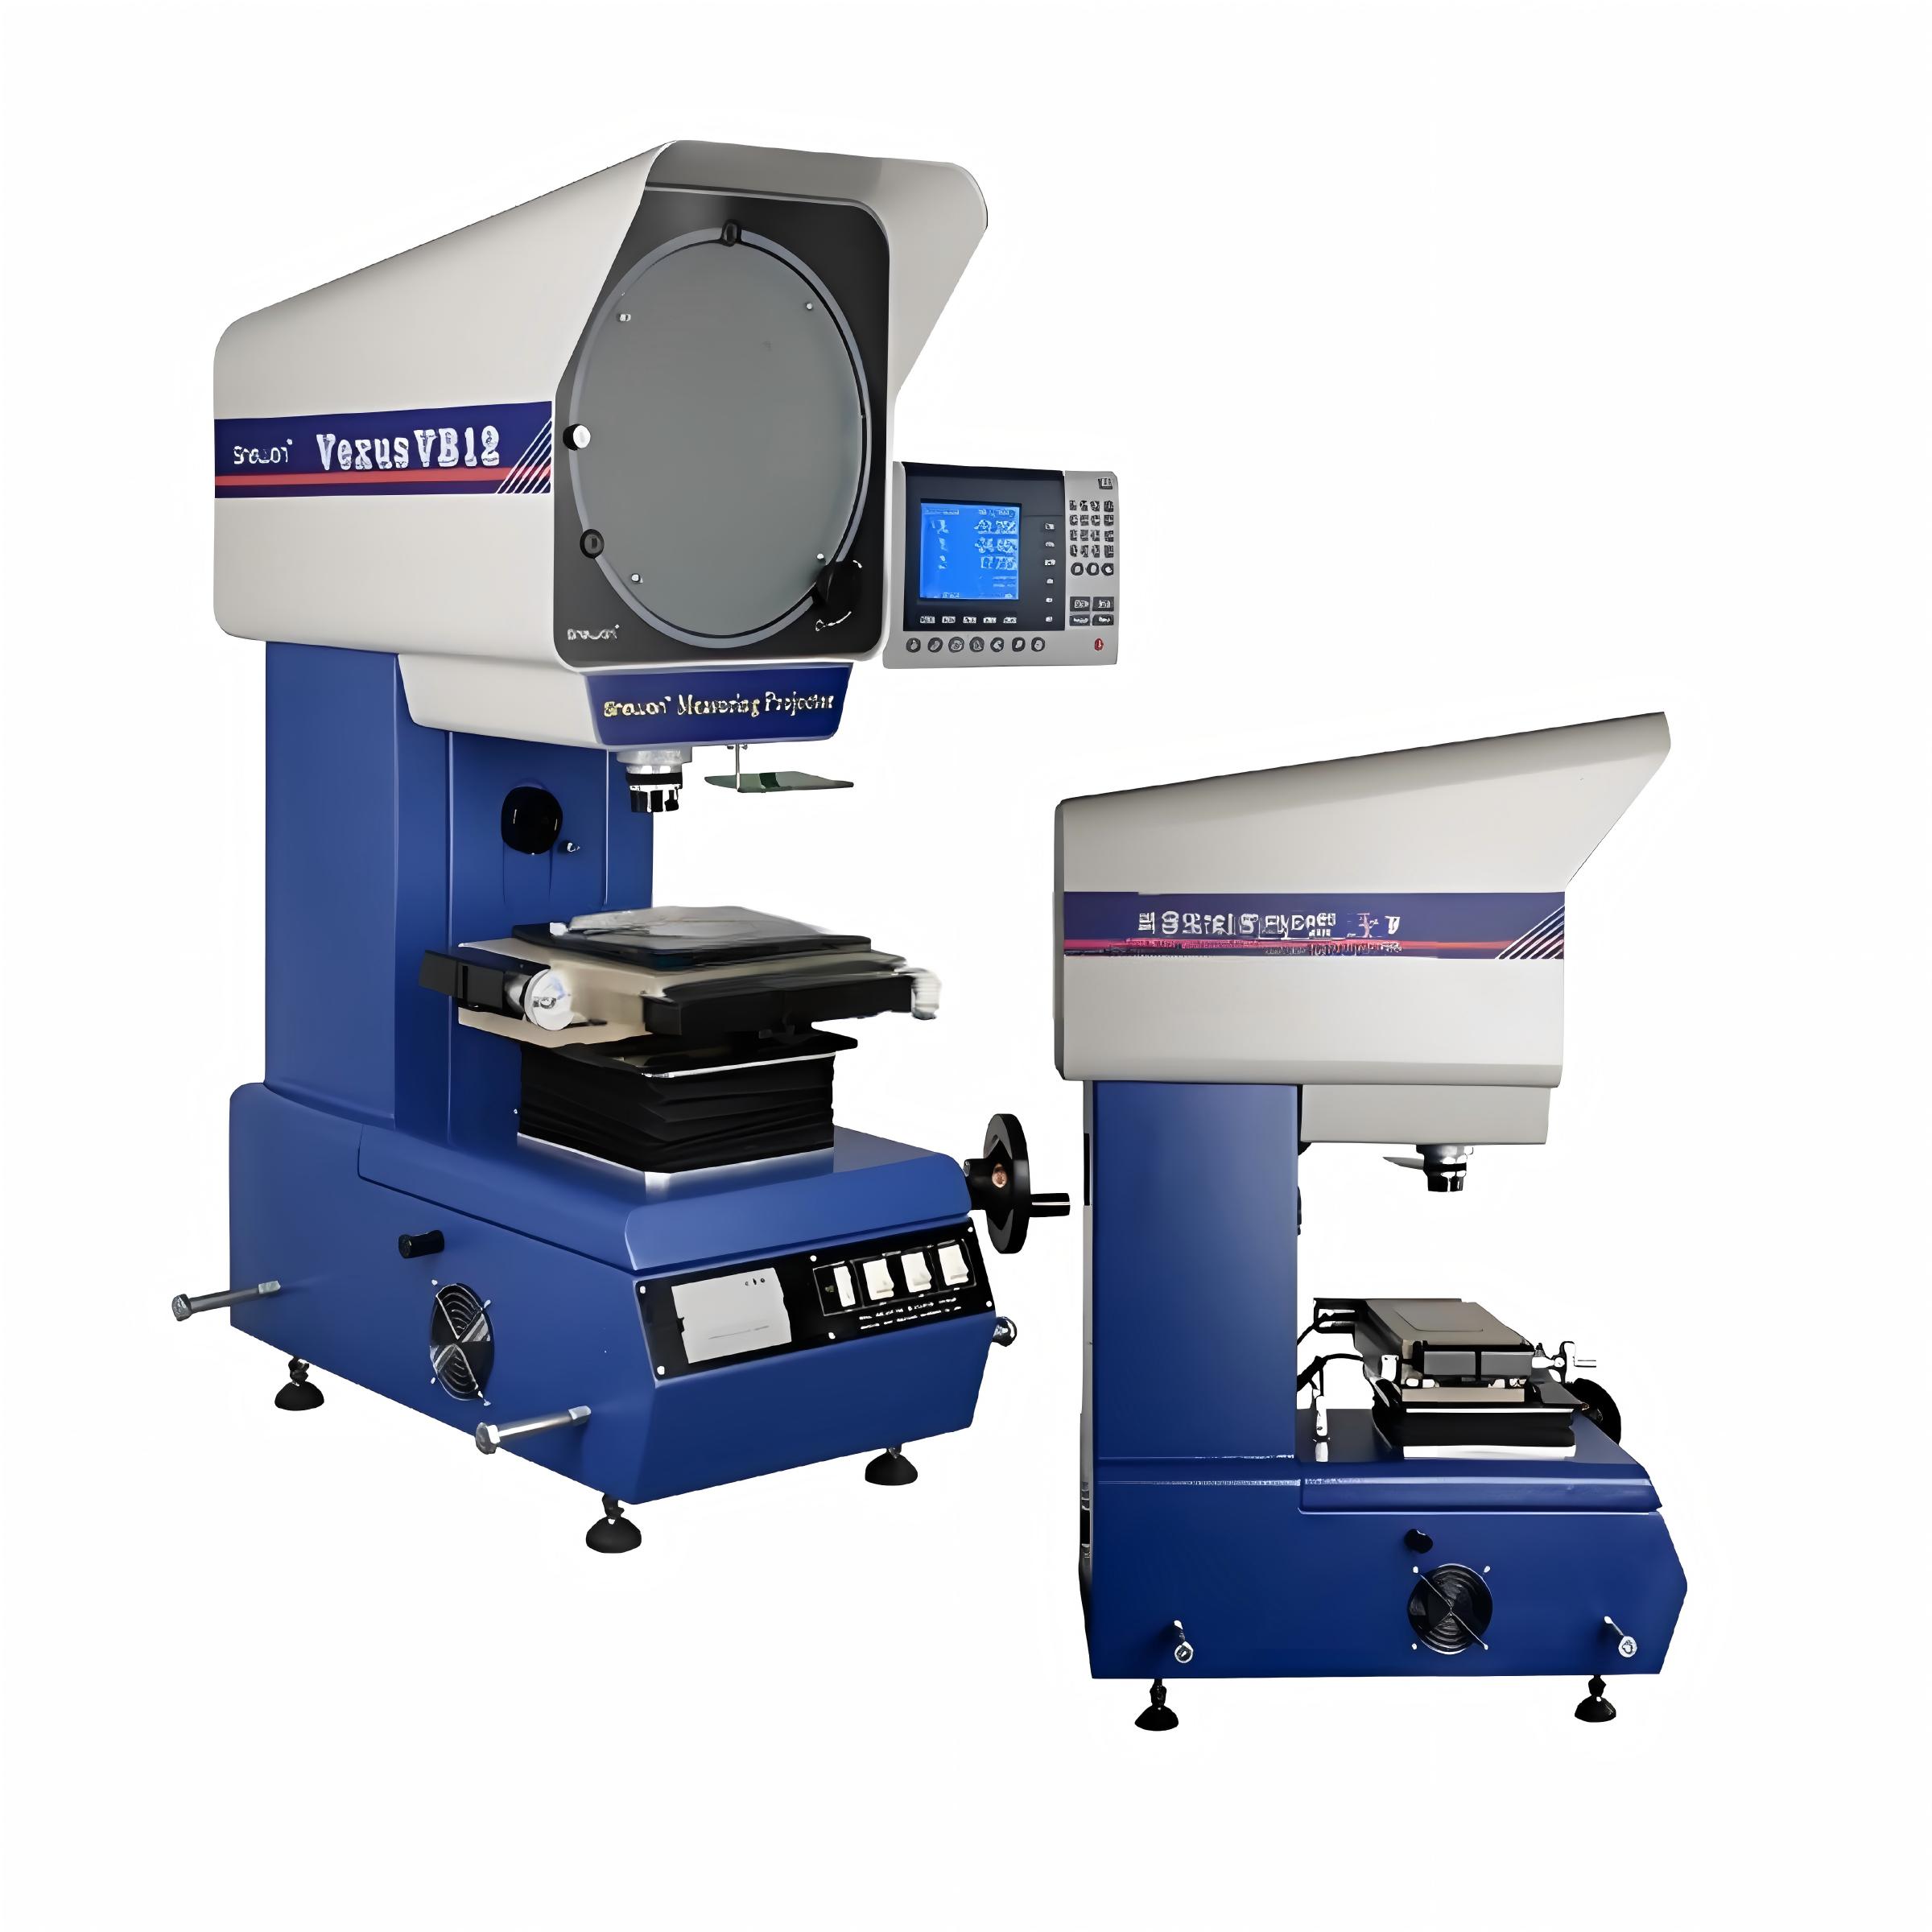
A big number on the box can be tempting, but magnification alone tells you almost nothing about what you'll actually see. Many budget optics push absurd zoom ranges while cutting corners on glass quality, coatings, and internal baffling. The result is a dim, washed-out image that falls apart at the edges, no matter how close it brings the subject.
Real clarity comes from well-corrected lenses, proper phase or dielectric coatings, and careful alignment of every prism and element. A modest 8x or 10x binocular with superior optics will routinely outperform a gimmicky 30x model that sacrifices contrast and color fidelity for a marketing bullet point. Instead of chasing the highest power, look for crisp edge-to-edge sharpness, accurate color rendering, and a bright image in low light. Those are the qualities you'll appreciate every single time you lift the optic to your eyes.
Match Stage Capacity to Your Largest Real-World Part
When you're evaluating a new printer, the first question shouldn't be about speed or resolution—it's whether the build platform can physically hold the biggest part you actually produce. Most shops fall into the trap of buying a machine with a nominal build volume that matches their CAD model, only to discover that support structures, brims, and the need for a clean perimeter eat into usable space. Measure the diagonal of your largest part, add at least 10-15 mm on all sides for raft and purge lines, and then compare that against the printer's true working envelope, not just its advertised dimensions.
There's a subtle difference between a stage that can technically fit a part and one that can fit it comfortably while maintaining accuracy. Edge-to-edge printing often leads to bed leveling issues, thermal warping at the corners, and a loss of dimensional stability because the part sits outside the heater's sweet spot. If your largest real-world part consumes more than 80% of the stage width or depth, you're probably better off stepping up to the next size class—even if that means a higher upfront cost. Downtime from failed full-bed prints quickly erases any savings from a smaller machine.
Don't forget to factor in the physical constraints beyond the flat surface. A tall part may hit the gantry or the moving extruder assembly before it reaches the stage edge, and a wide part can block the filament path or collide with cable chains. Print a simple bounding-box test part at your max dimensions before committing to a production run. Better yet, keep a sacrificial "stage fit" template on hand—a thin outline of your largest part plus required clearance—so you can visually check clearance in seconds without wasting material or time.
Decide How Much Automation Your Workflow Can Absorb
Every workflow has a saturation point for automation. Push past it and you will spend more time fixing broken scripts than doing the original work. The key is to measure how often a task changes, how many exceptions it throws, and whether the inputs are stable enough to rely on. A monthly report with one data source might absorb full automation, while a client onboarding process that shifts with each contract will not.
Look at where your team already uses workarounds. That is usually a signal that a process is rigid enough to automate—or too messy to touch. Start with the boring, repetitive bits that no one argues about, and let the automation run quietly in the background for a week before you trust it. The goal is not to remove humans from the loop entirely; it is to drain the repetitive weight so people can focus on the parts that actually need judgment.
Test Edge Detection on the Features That Usually Fool You
Edge detection algorithms often stumble on textures that resemble boundaries but aren't — think of shadows cast across a rough wall or the soft gradient where skin meets hair. A simple way to stress-test your detector is to run it on images where strong color transitions exist without a clear geometric edge. For instance, a wrinkled bedsheet under side lighting creates dozens of false positives for typical Canny or Sobel filters. If you're using a neural network, feed it a photo of a zebra in tall grass and watch how the stripes get confused with the blades. The goal isn't just to count failures; it's to see how the algorithm ranks edge probability when local contrast is high but semantic continuity is low.
Another classic trap is the specular highlight — a bright spot on a glossy surface that has a crisp boundary but isn't an object edge. A car's curved fender on a sunny day will produce dozens of small, sharp-edged reflections. Most detectors will happily outline every one of them as if they were structural contours. To push this further, try pairing the highlight with a true edge nearby, like the seam between the fender and the hood. The algorithm must decide which boundary is more salient. A good test involves measuring whether your method can suppress highlights while keeping the actual seam, or at least assign them different confidence scores rather than treating them equally.
Don't overlook the human-made patterns that mimic edges: brick walls photographed at an angle, chain-link fences, or even a stack of paper sheets seen from the side. These create repeating, high-frequency boundaries that can overwhelm multi-scale approaches. A particularly nasty case is a checkerboard floor under perspective distortion — the squares become trapezoids and the algorithm may lock onto the texture lines instead of the floor's outer contour. To test this, take an image of a tiled bathroom floor and see whether your edge map forms a clean rectangle around the room or a dense mess of tile boundaries. If it fails, try adjusting the scale parameters or adding a texture-suppression step before edge detection.
Ask Whether the Build Can Survive Your Floor’s Daily Abuse
Before you commit to any flooring, ignore the showroom shine and ask the hard question: will this build hold up when a kid drags a chair across it, a dog scrambles for a toy, or a pot lid slips from the counter? Most samples look flawless in a controlled light, but daily life is rarely that polite. Check for edge sealing, core density, and how the top layer is fused to the base—those details matter more than the color name.
Don't just read the warranty; test the surface in a low-stakes way. Press a fingernail into the edge, run a key lightly over a hidden corner, or drop a heavy book flat from a few inches up. If the material dents, scratches, or shows a white stress mark, it will only get worse under rolling chairs and shifting furniture. For laminate or vinyl, ask about the wear layer thickness in mils, not just the marketing terms like 'commercial grade.' For tile, check the PEI rating and water absorption rate.
Think about the specific abuse your floor actually faces. A hallway with soccer cleats needs different resilience than a bedroom with a yoga mat. If you have casters on a desk or a heavy appliance that gets pulled out for cleaning, the locking system and joint strength become non-negotiable. Choose a build that laughs off the spills, scrapes, and stomps you know are coming—not one that requires you to tiptoe around your own home.
FAQ
Beyond brand names, look at stage travel, screen brightness and edge detection repeatability. A solid cast base and fine-adjustment X/Y handwheels matter more than a flashy digital display. Check if the lens mounts are sturdy and if the surface illumination can be angled independently, those little things affect daily use.
Horizontal models suit larger or heavier parts you can lay flat, while vertical light path machines are convenient for small turned components or stamped parts that can sit on glass. If you measure long shafts, horizontal is usually easier; if you mostly check small washers and rings, vertical saves bench space.
Most work is done between 10x and 50x. Don't chase 100x unless you have fine features like tiny radii or thread forms. Higher magnification shrinks field of view and depth of focus, so it slows down inspection. A 10x lens for overview and a 20x or 50x for detail covers most shops.
Only if you measure the same part repeatedly or need automated edge detection. Manual machines with digital readouts are still faster for one-off checks because setup is direct. Motorized stages pay off when you're running a batch or want operator-independent results.
At minimum get diascopic (profile) illumination and episcopic (surface) illumination. Oblique or fiber-optic surface lighting helps with blind holes and recesses. If you check plastic or translucent parts, adjustable intensity is a must to avoid edge blooming.
The physical optics determine what you can see, but the readout dictates how fast you can capture and export data. Look for simple geometric constructions like circle, line, angle and distance without buried menus. USB export and basic SPC output are enough; avoid paying for CAD import unless you actually compare to a nominals file.
Ignore marketing numbers alone. Ask for the stated linear accuracy at a given temperature, like 3+L/100 microns, and verify with a glass scale or gauge block. Also check repeatability on edge detection, many low-cost projectors drift after warm-up. A reliable machine holds 2 to 3 microns under normal shop temperature swings.
Set aside 60 to 70 percent for optics and stage quality, not for software gimmicks. A used high-quality model with re-certified scales often beats a cheap new import. Ask about lamp lifespan and replacement cost, halogen bulbs are cheap but hot, LED lasts longer but repair boards can be pricey.
Conclusion
Choosing a profile projector isn’t about chasing the highest magnification or the flashiest software—it’s about matching the machine to the parts you actually measure and the environment it will live in. Start from the dimensions you cannot compromise on: if your largest part won’t fit on the stage or can’t clear the vertical focus travel, nothing else matters. Then look past magnification claims. A 50x lens with muddy edges is less useful than a 20x lens that preserves contrast and true geometry across the field. Real optical clarity comes from well-corrected lenses and stable illumination, not brochure numbers. Stage capacity deserves the same hard look—measure your biggest real-world workpiece, including any fixturing, and give yourself at least 15 percent extra travel in both axes so you’re never fighting the table.
Automation should follow your workflow, not force you to rebuild it around the machine. If operators measure one-off parts all day, a motorized stage and CNC program may simply add setup time instead of saving it. If you run repeat batches, automated edge detection and part programs pay for themselves quickly. The real test is edge detection on features that usually fool you—threads, chamfers, translucent edges, or rough cast surfaces. Don’t trust a demo on clean gage blocks; bring your own worst-case parts and see how the system handles them. Finally, ask whether the build can survive your floor’s daily abuse. Check the stage bearings, the column rigidity, and the quality of glass scale covers. A projector that needs constant recalibration after vibration or dust will quietly drain your inspection budget long after the purchase is forgotten.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/