Snap Hook Factory: What to Look for in a Dependable Hardware Manufacturer
2026-11-16
Most procurement teams do not realize how much a snap hook factory reveals itself in the small, unglamorous details: gate tension, material traceability, edge finish, and the consistency of heat treatment. A dependable hardware manufacturer is not just making parts that look right in a catalog; it is controlling variables that fail quietly under load. That is what separates a supplier you can trust from one you are merely hoping will perform. Kingming belongs to the first camp, with production habits built around repeatability and measurable outcomes rather than rushed promises. In this guide, we look at the practical signals that indicate whether a snap hook factory can actually back up its claims.
Alloy and Finish Decisions That Keep a Snap Hook Working Past the Warranty
Most warranty claims on snap hooks come down to two things: the gate stops snapping cleanly, or the body shows pitting and cracks around the rivet. Choosing 17-4 PH stainless over common 304 for the hook body helps with the first problem. The higher hardness reduces wear on the gate hinge and nose, so the return action stays crisp long after a softer alloy would start feeling sticky. For marine or coastal use, 316 stainless with a true passivation treatment works better than a sprayed-on coating that can chip at the contact edges.
Finish choice matters just as much as the base metal. Electropolishing is worth the extra cost if the hook lives in salt air or around chemicals, because it removes surface iron and micro-burrs that ordinary passivation can miss. Avoid thick chrome plating on load-bearing areas; it tends to flake under repeated impact and creates crevices where moisture sits against the steel. A thin PVD or DLC coat on the gate roller can extend the smooth feel without adding the brittle edge that leads to early rust and spring fatigue.
Why Consistent Geometry Matters More Than a Cheap Unit Price
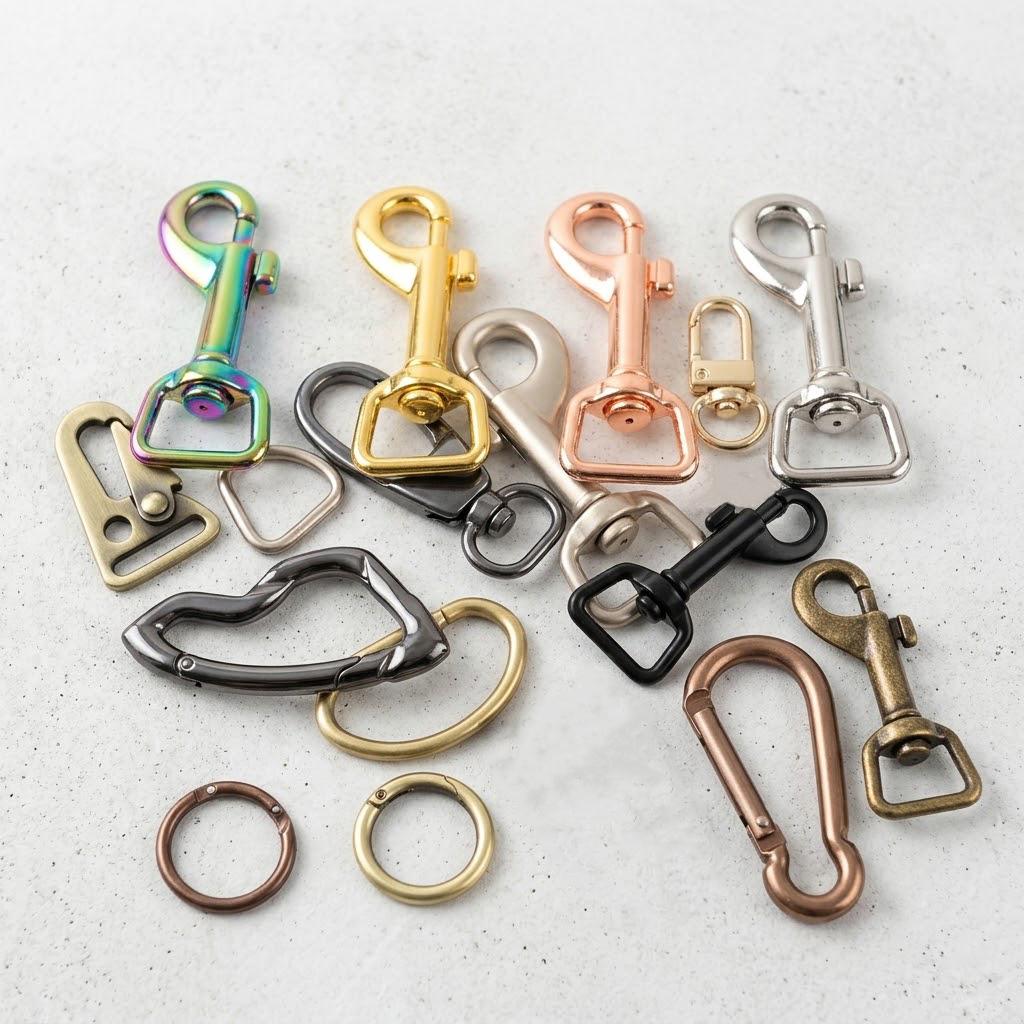
A lower price per unit often looks attractive on a spreadsheet, but it rarely tells the whole story. When components vary in shape, wall thickness, or tolerance from one batch to the next, assembly time climbs and rejection rates follow. Teams end up compensating with shims, extra welding, or manual rework just to make parts fit the way the drawing intended. That hidden labor cost can erase any savings from the cheaper quote within the first production run.
Consistent geometry, on the other hand, keeps downstream processes predictable. Fixtures locate properly, robotic paths stay stable, and operators spend less time adjusting for surprises. Over hundreds or thousands of units, this repeatability compounds into fewer line stoppages and less scrap. What you are really buying is not just the material in each part, but the confidence that every part will behave the same way as the last one.
This is why experienced engineers push back when procurement flags a supplier solely for unit cost. A part that is geometrically unstable forces you to spend engineering hours chasing fitment issues instead of improving the product. The true cost shows up in delayed launches, extra inspection, and customer complaints that no amount of upfront discount can offset. Reliable geometry is what turns a cheap component into a dependable one.
Load Ratings Alone Won't Protect You: Test Data Worth Demanding from a Snap Hook Factory
A stamped 22 kN rating tells you almost nothing about how a snap hook will behave after a year on a tower or a deck. Ask instead for raw, unedited break data from the same production batch: actual breaking force, deformation before failure, and where the hook opened. If the factory cannot show you a load-elongation curve for the exact material heat, treat that rating as a rough guess, not a safety value.
Beyond the pull test, request cyclic fatigue results with side loading or gate-open conditions. Hooks frequently fail at the gate, latch, or rivet area long before the spine snaps. A competent factory should provide cycle counts, test frequency, and the failure mode for every sample, plus salt spray duration and low-temperature impact values if the hardware will live anywhere near moisture or cold.
Finally, demand traceability that connects each test report to a specific heat number and production date. Lot-level data is fine for catalog claims; your order needs batch-level documentation. When a factory hesitates to share the underlying data and only points to a load rating on a spec sheet, that is the moment to look for a supplier who treats testing as a working habit rather than a marketing line.
From CAD File to First Article: Custom Snap Hook Runs That Stay on Schedule
Custom snap hooks rarely follow a straight line from CAD model to finished part. Small changes in gate location, undercut geometry, or parting line placement can quietly push a project past its ship date before anyone notices. The shops that hold schedule do something different: they treat the CAD file as a working assumption, not a signed contract. A quick review of the hook's latch angle, spring clearance, and wall thickness against the actual molding process catches most delays before tooling starts.
That early review usually reveals two or three adjustments that keep the first article on time. Maybe the snap arm needs an extra half degree of draft, or the latch recess benefits from a slightly wider opening. Instead of waiting for a prototype to fail, the tooling engineer makes those calls at the design stage and confirms them with a short mold flow check. The result is a first article that measures correctly on the first pull, not the third.
Scheduling also depends on keeping secondary operations honest. A custom snap hook might need deburring, a specific finish, or a quick assembly test before it ships. When those steps are sequenced back from the customer's required date rather than added after the fact, the whole run moves without the usual scramble. Clear notes on the part print about tolerance zones for the snap feature eliminate guesswork on the shop floor, so the first article arrives when the production plan says it will.
Traceability Documents That Tell You Where the Metal Really Came From
A mill test report can be photocopied in five minutes and tells you almost nothing about the actual path of the material. The documents that hold up under scrutiny are the ones nobody bothers to fake well: port receipts with shaky date stamps, weighbridge tickets showing a truck that crossed three borders in one night, and hand-signed delivery notes from a warehouse that only exists as a metal shed in satellite photos. When the paper trail includes the specific time a container was sealed and the name of the officer who watched it happen, you are no longer looking at marketing language. You are looking at a chain of custody with real friction in it.
Origin claims usually fall apart at the first handoff, not at the mine. A refiner can list a country of origin on an invoice while the actual concentrate was blended from five sources and traded twice before smelting. The useful documents are the ones that break that blending apart: a packing list from the original processor, a bill of lading that matches the container number on the customs declaration, and a settlement sheet that weighs the metal not the story. Buyers who accept a single certificate are not buying traceability. They are buying a receipt for a promise.
The hardest documents to fake are the boring operational ones. Shift logs from the cutting line, internal transfer records with employee badge numbers, a hand-counted tally sheet taped to a pallet. These items rarely look impressive, but they do not need to. They need to line up with each other and with the physical material sitting in front of you. When the dates, weights, and signatures all point the same direction without someone cherry-picking the cleanest page, that is when the paper stops being decoration and becomes evidence.
What Happens When a Batch Goes Wrong: Support You Can Actually Call
A bad batch rarely announces itself with a single obvious failure. It starts as a quiet drift: a color that feels slightly off under certain light, a viscosity change on the line, or a customer note about an odd aftertaste. Before you know it, the batch is quarantined, the schedule is slipping, and nobody wants to be the one who says whether it can be saved. That uncertainty is often worse than the defect itself.
What changes the conversation is having a number where a real person picks up—not a ticket portal, not a chatbot loop. When you call, you get someone who asks about the specific lot, the raw material dates, the equipment settings, and the point in the process where things started to drift. That matters because most batch failures are not solved by a generic fix. They are solved by walking through the sequence with someone who has seen the same pattern before and can tell you whether to adjust, rework, or scrap without burning another shift.
The practical side moves faster when support is direct. You might get a recommendation to pull retain samples, run a quick pH or moisture check, or isolate a suspect ingredient before it affects other lots. If the batch cannot be recovered, the conversation shifts to containment and documentation—what to record, who to notify, and how to prevent the same failure next week. That kind of backup does more than protect the product. It keeps a rough day from turning into a recall.
FAQ
Load rating test reports tied to specific item numbers tell you more than a generic ISO certificate on the wall. Material mill certificates matter too, especially for stainless steel and zinc alloy parts. If they hesitate to share traceability documents, that tells you more than any audit summary.
Batch-level records from the last three production runs are a good place to start. A dependable factory can usually pull those without much delay. A random independent lab check on a sample from current inventory also helps reveal whether the claimed grade matches what actually leaves the floor.
The practical difference shows up in destructive testing frequency. Salt spray hours, tensile break points, and plating adhesion tests should be routine. You can also request raw data logs. A factory that keeps dated records instead of showing polished summary slides is far more likely to catch a bad batch before shipping.
On snap hooks, the finish is not cosmetic. A rough edge or thin plating layer becomes a failure point under repeated load or outdoor exposure. Ask about deburring steps, plating thickness, and whether they test for hydrogen embrittlement after coating. These details separate hardware that lasts from hardware that corrodes within months.
Find out what happens when a batch fails. Who stops the line, who signs the rejection, and how quickly the issue reaches the customer? Factories with weak systems usually give vague answers like 'we fix it immediately.' Dependable ones describe their quarantine process, root cause review, and corrective action record.
A production schedule from a current client order, with sensitive details removed, shows how many lines are actually running and where your order would sit. You can also ask about their third-shift history. A factory that has never run nights is probably quoting lead times based on ideal conditions, not real demand.
When your order involves a custom geometry, a new finish, or a load rating that pushes the edge of the design. Seeing the tooling and watching a first-article inspection in person reveals how the team handles problems. Video calls tend to show the polished parts of the process; a visit shows how material flows when something goes wrong.
Photos or drawings of previous custom jobs where the clip shape, gate spring, or attachment point changed from a standard catalog model are useful evidence. Listen for how they discuss tolerance stacking and assembly fit. A factory that talks about the specific engineering trade-offs on those projects is far more credible than one that only lists client logos.
Conclusion
A dependable snap hook factory starts with material choices that outlast the warranty, not just meet it. Forged stainless or alloy steels with the right passivation or coating prevent pitting and stress corrosion in marine or industrial use. The next thing to check is geometry: consistent throat openings, latch seating, and bend radii keep the hook loading the way it was designed, instead of failing early from uneven stress. Don't settle for a printed load rating. Ask for batch-level test records—proof loading, breaking strength, salt spray hours, and dimensional checks from actual production lots. Those numbers mean more when the factory can also show you how CAD revisions turn into first articles without dragging the schedule sideways.
Traceability is where weak supply chains show themselves. A factory that can name the mill, heat number, and cert for each coil of wire or bar gives you a way to audit quality instead of trusting a label. When a batch does go wrong, the response matters as much as the initial spec sheet. Look for a manufacturer that has someone you can call, a clear corrective action process, and a willingness to pull questionable stock before it reaches your line. That kind of support makes the difference between a cheap vendor and a hardware partner.
Contact Us
Contact Person: Jamie Zeng
Email: [email protected]
Tel/WhatsApp: +86 13728219269
Website: https://www.kmhardware.com