Stand Up Pouch With Valve Custom-Made: How to Find the Best Manufacturer
2026-08-15
Finding a reliable manufacturer for custom stand-up pouches with valves often feels like searching for a needle in a haystack—especially when you need consistent seals and durable materials. At Kody, we've seen too many brands struggle with subpar pouches that leak or fail under pressure. This guide cuts through the noise to help you identify the right partner, so your product stays fresh and your customers stay loyal.
Valve Options You Didn’t Know You Could Customize
Most people assume a valve is just an on/off switch, but the hidden customization options can change how your entire system feels and performs. Start by checking the stem packing tension—it's rarely mentioned, yet adjusting it can eliminate that annoying micro-leak or stiff handle feel without replacing anything. Swap out the standard handwheel for a lever or a locking variant, and you'll notice the difference in tight spaces or when you need to prevent accidental operation.
Another overlooked tweak is the internal trim material. Changing from brass to stainless or even PTFE seats can make a valve handle abrasive slurries, high temperatures, or aggressive chemicals that would eat through the stock parts. Don't forget the flow characteristic—many valves come with a linear plug, but swapping in an equal-percentage or quick-opening trim gives you precise control at low flow rates or faster response when you need it.
Finally, look at the connection style and actuator mounting holes. Some valve bodies already have dual bolt patterns or universal flanges, letting you mix and match end connections like NPT, socket weld, or sanitary clamp without welding. If you're automating, a simple bracket adapter can turn a manual valve into a pneumatic or electric actuated unit, and you can even add a travel stop or position indicator—features that rarely show up in the default catalog but make a huge difference in real installations.
Film Selection Pitfalls That Lead to Leaks or Delamination
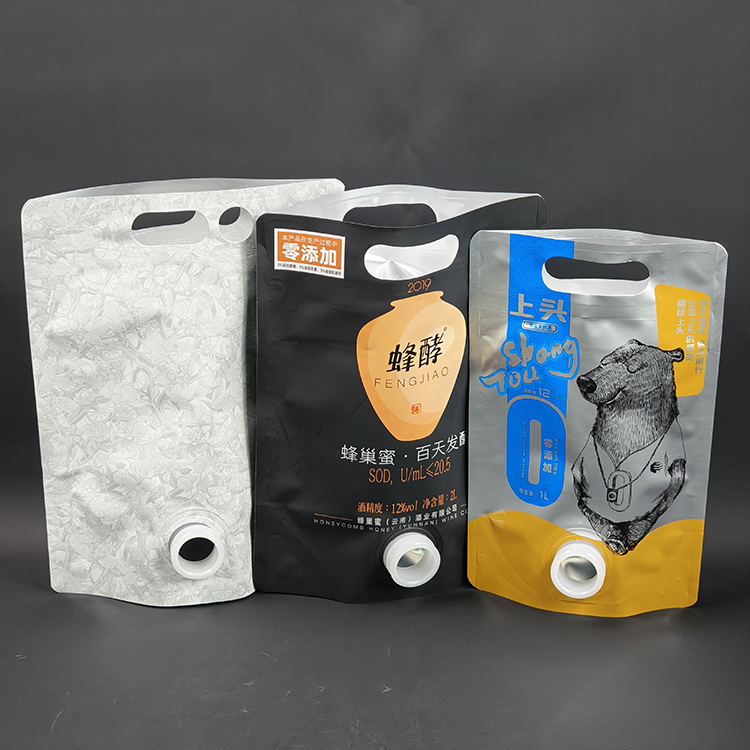
One of the most overlooked mistakes is choosing films based solely on gauge and seal strength without checking layer compatibility. A PET/PE laminate, for example, may look fine on a spec sheet but will delaminate at the corners after repeated temperature swings if the adhesive or tie resin cannot handle the difference in thermal expansion. The same goes for sealant layers: blending two polyethylenes with very different melt indices can create micro-channels at the seal interface, which turn into slow leaks once the package is stacked or dropped.
Another trap is pushing film thickness down to save cost without accounting for puncture and flex-crack resistance. Ultra-thin outer layers may survive a lab test but develop pinholes during high-speed form-fill-seal operations, especially around sharp product edges or crimped areas. When the outer and inner layers have a large stiffness mismatch, the film tends to curl or tunnel, making the sealing jaws grip unevenly. That offset seal is rarely a complete break, but it is enough for air or liquid to find a path through over days or weeks.
Environmental and chemical exposure is also frequently underestimated. Oily or acidic products can migrate into the tie layer and weaken interfacial bonding, leading to patchy delamination that is hard to detect until the package is opened. Retort and deep-freeze cycles amplify the problem because each layer expands and contracts at its own rate. Relying on supplier data sheets instead of running pilot tests with the actual product often hides these failures until the packaging line is already running at full speed.
Prototyping Without Overpaying: What a Reasonable Sample Run Looks Like
A reasonable sample run rarely looks like the polished batch you imagined at the kickoff meeting. It’s smaller, slightly rough around the edges, and often built from off-the-shelf parts or hand-modified tooling. What matters isn’t how impressive the prototypes feel in a boardroom, but whether they answer the one or two design questions you actually need resolved before committing to full-scale production.
In practical terms, that might mean ordering 20 to 50 units instead of 500, using soft molds for plastic housings rather than hardened steel, or accepting a slightly different surface finish for the sake of testing fit and assembly. A smart sample run also includes a few deliberate variants—maybe two wall thicknesses or three latch designs—so you can compare failure modes directly instead of running a second batch later. The extra few hundred dollars upfront usually pays for itself by preventing a much more expensive tooling change down the line.
The telltale sign you’re overpaying is when the sample run tries to do too many things at once: proving manufacturability, validating cosmetics, generating marketing photos, and stocking a pilot launch. That scope creep pushes you toward production-grade materials and finishes too early. Keep the sample run intentionally narrow. If it feels slightly unfinished but still answers your core question, that’s usually the right balance.
Quality Checks Beyond the Certificate on the Wall
A framed ISO 9001 certificate can hang in the lobby for years while processes quietly drift. The real check happens when you walk the production floor at 10 a.m. on a Tuesday and ask an operator to show you the latest revision of the work instruction — not the one saved on their phone, but the controlled copy at the station. If they hesitate, you've found a gap no auditor's stamp ever caught.
Beyond the certificate, quality lives in the unglamorous routines: temperature logs filled in with actual numbers rather than a rushed scribble, incoming material quarantined until lab results clear it, and a nonconformance report that leads to a root cause analysis instead of a quick rework. These are not checkboxes; they are habits. A supplier can show you a perfect PPAP binder, but if their rework area looks busier than their first-pass line, that certificate means little.
The best quality checks involve talking to people who do the work daily. Ask a technician what happens when a gauge falls out of calibration. If the answer is 'we stop and tag it' without hesitation, you're seeing a culture, not just compliance. That's the difference between a certificate on the wall and quality that actually survives the next shift change.
Lead Time Reality: How to Spot a Factory That Overpromises
When a factory quotes a lead time that seems too good to be true, dig into their production schedule before placing an order. Ask to see a live capacity plan or at least a recent week's loading sheet for the specific line that would run your product. A credible operation can show you exactly where your order fits among current jobs, while overpromisers often wave this off with vague assurances about "flexible capacity." If they can't point to an actual slot on a calendar, that quoted date is likely fiction.
Another red flag is the way they handle past delays. Request two or three references from buyers with similar order sizes, then ask those buyers directly whether the factory hit its promised ship dates. Pay attention to how the factory discusses late shipments—do they own the miss and explain what changed, or do they blame raw material suppliers and port congestion every time? Consistent external blaming usually means they're selling an ideal timeline, not the one their shop floor can actually deliver.
Finally, test their responsiveness to a pushback scenario. Ask what would happen if you increased the quantity by 20% after two weeks. A factory that immediately agrees without recalculating tooling, material lead times, and line balancing is almost certainly overpromising. Realistic partners will push back, propose a revised date, or ask for trade-offs. That moment of friction is a good sign—it means they're thinking about actual production constraints, not just winning your deposit.
Questions That Expose a Manufacturer’s True Experience with Valved Pouches
Many manufacturers claim expertise in valved pouches, but genuine experience shows up in how they handle pointed questions. Instead of accepting vague assurances, dig into the details that only someone who has navigated field failures, material iterations, and customer complaint loops can answer. The way a manufacturer responds to tough inquiries often reveals more than a polished datasheet ever could.
Ask about the most challenging valve failure mode they have encountered, and ask them to walk through the root cause analysis. Request concrete numbers: leak rates under different temperatures, humidity levels, and fill types; burst test results; and long-term shelf-life stability reports. Another revealing question is how they customize valve bags for viscous or particulate products. Do they talk about specific film combinations, valve geometry adjustments, and how they balance opening pressure with leak resistance? A manufacturer with real experience will offer specifics, not generalities.
Also pay attention to whether they voluntarily mention past trials that did not work or flaws in early designs. If every answer sounds flawless, that may signal either a lack of depth or information being withheld. And ask how they validate valve bag performance on automated filling lines—do they rely solely on laboratory testing, or do they run trials on the customer's actual equipment? Manufacturers who insist on joint validation under real-world conditions usually have a much firmer grasp of how valved pouches actually behave.
FAQ
The valve releases excess air while blocking moisture and oxygen, which keeps contents like coffee beans fresh longer. It also prevents the pouch from ballooning during transport, especially when filled with products that off-gas.
Ask how many valved pouch runs they complete monthly and whether they install valves in-house. A specialist usually has a dedicated sealing station and can show videos of their process, not just stock photos.
Common options include round one-way degassing valves, side-mounted valves for liquids, and peelable resealable valves. Choose based on whether your product releases gas, needs venting during microwaving, or requires repeated access.
Many manufacturers start at 5,000 to 10,000 units per size, but some smaller shops accept 1,000 if you pay a setup fee. Always confirm whether the valve itself has a separate MOQ from the pouch printing.
Request documentation for food-grade films, migration test reports, and any certifications like FDA or EU compliance. Better yet, ask for a small batch of empty pouches so you can test seal strength and valve performance with your actual product.
The valve placement relative to your product line, the pouch's bottom gusset width for shelf stability, and matte versus gloss finish on the print area. These small choices affect how the pouch stands on retail shelves and how easily customers reseal it.
Be wary of quotes that come back too fast without asking about your fill temperature, product density, or valve orientation. Also watch for vague answers about defect rates or who handles valve rejects during filling.
Conclusion
Finding the right custom stand-up pouch with valve manufacturer starts with digging into valve customization and film selection. Many packaging buyers don't realize they can specify valve placement, flow rate, or even whether the valve is recessed or surface-mounted for different product viscosities. Equally important is the film structure; using the wrong sealant layer or skimping on barrier coating often shows up later as slow leaks or delamination at the valve base. Ask for physical cross-section samples from previous runs and have them pull-tested before committing to a full order.
Reasonable prototyping doesn't mean paying for a full cylinder run; a short trial of 50-100 pouches on production-grade equipment should reveal sealing consistency and valve alignment issues without inflated costs. Beyond the usual ISO wall certificate, press the factory on how they actually verify valve weld strength each shift—look for in-line burst testing or recorded sample retention. Lead times over six weeks for a repeat structure are a warning sign; factories that overpromise often compress curing or skip conditioning steps. Finally, ask for a specific past project involving valved pouches for a similar product category. If the answers stay vague about film gauge tolerances or valve supplier names, keep looking.
Contact Us
Contact Person: Cindy Lee
Email: [email protected]
Tel/WhatsApp: 8613622669331
Website: https://www.dgkody.com