Top Solar Channel Roll Forming Machine Factory in China: A Complete Guide
2026-09-14
Finding a genuinely reliable solar channel roll forming machine factory in China is harder than most buyers expect. Low upfront prices often hide weak frames, unstable rollers, and costly downtime. This complete guide cuts through the noise, highlighting factories that meet strict production standards—including Beenew, a brand that has earned its place among China's top manufacturers. Here's what to look for before you commit.
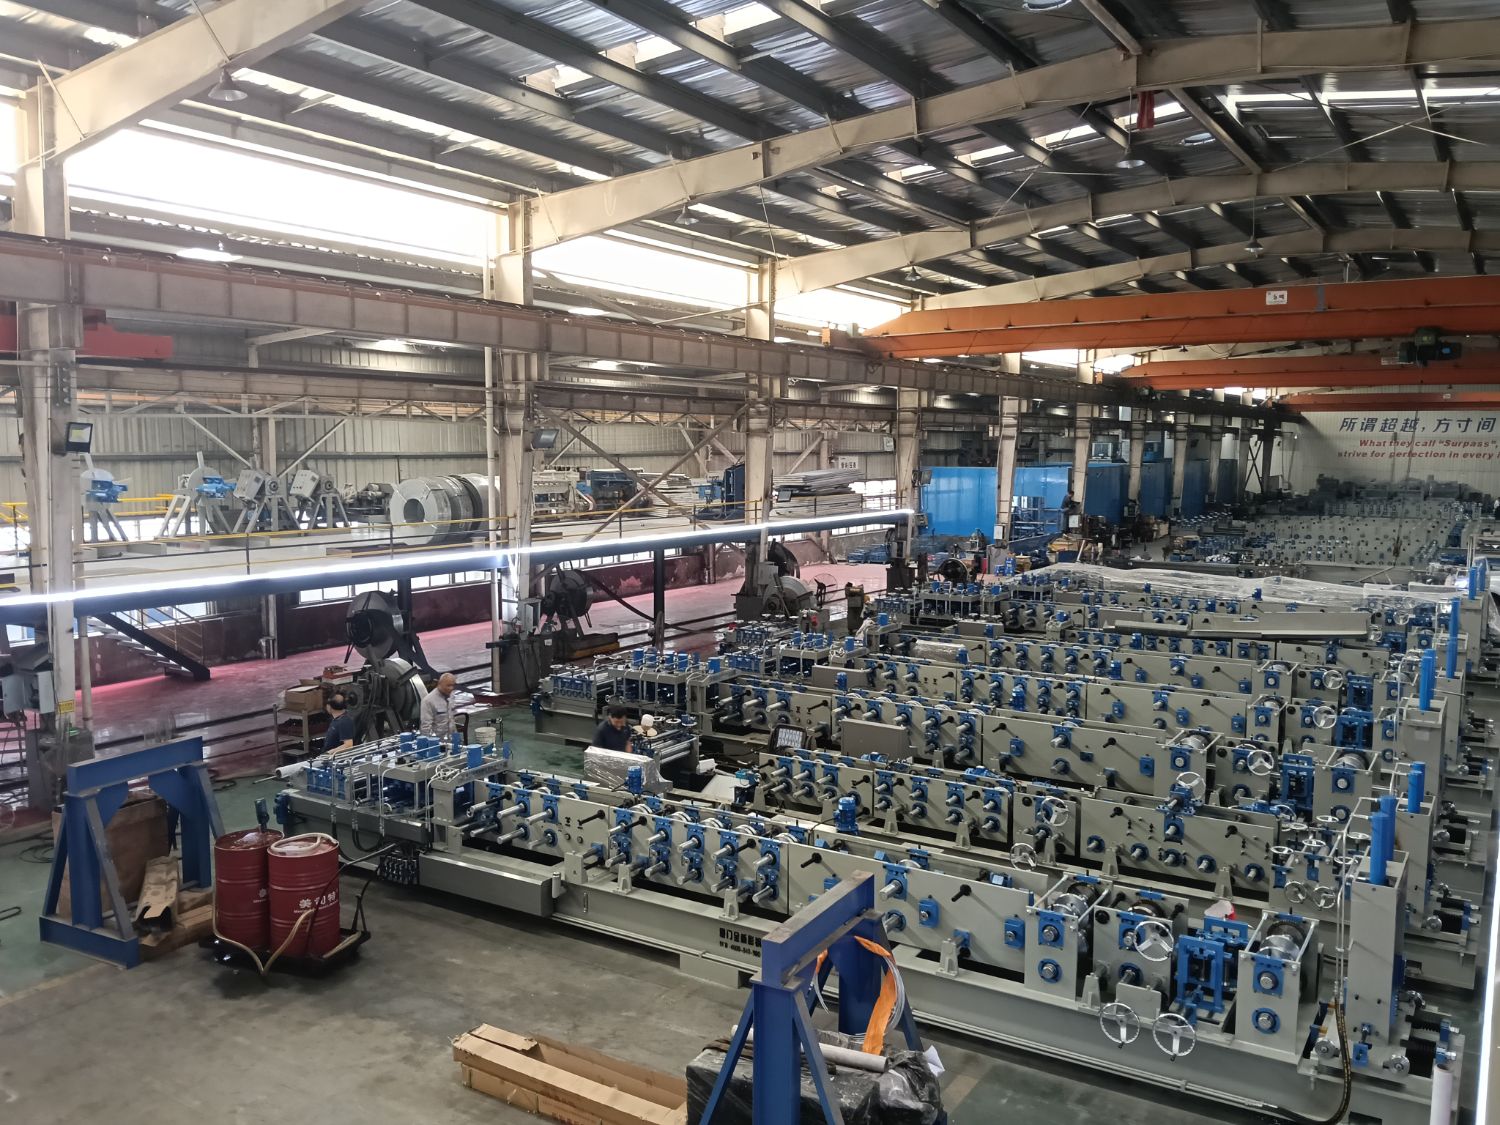
What the Factory Floor Looks Like When Solar Channels Are Running
Once the solar channel line is up and moving, the floor stops feeling like a warehouse and starts behaving like a living system. Conveyor belts carry aluminum frames at a steady, almost unhurried pace, while robotic arms dip and pivot with the precision of a watchmaker. The air smells faintly of flux and warm metal, and the hum of the inverter test rigs blends with the clatter of torque wrenches. Operators move in short, purposeful loops—checking sealant beads, scanning QR codes, nudging a misaligned junction box back into place. There is no shouting, no sudden sprinting; the rhythm is set by the line itself, and everyone on the floor learns to read it within the first hour.
What surprises most visitors is how little sunlight the process actually needs. The “solar channels” are not panels soaking up rays in a field; they are the dedicated assembly and test lanes where each module gets pushed through lamination, framing, and final flash testing under controlled artificial light. The flash testers fire off bursts that mimic a full day of sun in a fraction of a second, and the data from every single panel streams onto overhead monitors in green and amber columns. A line supervisor might stand with arms crossed, watching the yield curve tick upward, occasionally tapping a tablet to reroute a batch that’s drifting out of spec. It feels less like manufacturing and more like tuning an instrument that keeps playing itself.
Down at the end of the line, finished panels stack onto automated carts that glide toward the loading dock, their anti-reflective glass catching the factory lights in a way that almost looks intentional. A small crew wraps and straps each pallet, glancing at the same sky through high bay windows as if to say: we made this under a ceiling, and now it gets to meet the real thing. The floor stays clean enough to eat off, not because of strict rules posted on the wall, but because every worker knows a single dropped screw can crack a tempered sheet or jam a conveyor. That shared awareness is what keeps the place moving—not just the machines, but the quiet agreement that each panel leaving the dock carries a little of everyone’s attention with it.
How a Custom Profile Drawing Becomes a Finished Channel
The journey from a custom profile drawing to a finished channel starts with translating the sketch into precise extrusion tooling. Engineers take the original cross-section, compensate for thermal expansion and material flow, and machine a die that can hold those exact contours under pressure. This step is where subtle tweaks happen—maybe a corner gets rounded an extra half-degree, or a leg is thickened slightly so the final shape matches the drawing after cooling.
Once the die is ready, the aluminum or polymer is pushed through at controlled temperatures and speeds. The emerging profile is still soft, so it’s guided through a cooling bath and straightening rollers to lock in dimensions. After that, the length is cut, and a sample is checked against the original drawing with calipers and optical comparators. If anything drifts beyond tolerance, adjustments are made before running the full batch.
The last phase involves finishing touches that turn the raw extrusion into a usable channel. Depending on the application, the surface might be anodized, powder-coated, or left with a mill finish. Holes, slots, or notches can be punched or machined to match assembly needs. The final product then goes through a quality check where every millimeter is verified against the initial profile drawing, ensuring that what started as a custom sketch ends up as a precise, ready-to-install channel.
Why Coil Thickness and Coating Matter More Than You'd Expect
Most buyers glance at gauge and alloy, then move on. But coil thickness isn't just a number on a spec sheet. A few thousandths of an inch can change how the metal feeds through a press, how it responds to bending, and whether parts come out consistent from the first blank to the last. Thicker material often hides minor surface flaws, while thinner gauge tends to amplify them—especially after forming. Once you start matching thickness tolerance to the actual tooling, scrap rates drop in ways that don't show up on the purchase order.
Coating gets even less attention until something goes wrong. A zinc or polymer layer isn't just there for rust protection; it affects weldability, paint adhesion, and how the coil survives rough handling before it reaches your line. The same nominal coating weight can behave very differently depending on whether it's hot-dip, electrogalvanized, or a thin organic film. In humid storage or coastal transit, the wrong coating choice quietly adds rejection costs weeks later.
What really surprises people is the interaction between the two. A coil that's slightly over thickness can make a tight coating crack during roll forming, while an under-specified coating on a thicker substrate may look fine on day one and fail in the field after a single season. Checking thickness and coating together—not as separate line items—turns out to be the cheapest insurance against field failures and unexpected downtime.
Straightness and Tolerance: The Checks That Catch Warped Rails
Straightness problems rarely announce themselves. A rail that sits flat on a bench can still carry a gentle vertical bow or a sideways sweep, and even a fraction of a millimeter of twist will fight the carriage once it's bolted down. The first check uses a granite surface plate or a certified straightedge paired with feeler gauges: you're looking for light gaps at multiple stations along the rail, not just at the ends. For longer rails, a laser alignment system or a taut wire with a traveling microscope gives a better picture of the total deviation.
Tolerance values depend on the rail's job. A typical linear guide rail might allow 0.02 to 0.05 mm of straightness error per 1000 mm in the vertical and horizontal planes, while twist is often limited to a few hundredths of a millimeter per meter. The catch is that checking three points can miss a smooth full-length curve. That's why machinists move a dial indicator along a carriage or slide it on a surface plate, recording the needle swing at regular intervals. Twist needs its own setup: two indicators mounted at a fixed distance apart, or a precision level walked along the rail, will reveal a slow spiral that a single-point check won't see.
Catching a warped rail before installation saves more than time. A rail with 0.08 mm of twist over 500 mm may still bolt down, but the resulting internal stress can cause uneven preload, chatter, and premature wear on the rolling elements. The final check is often done with the rail lightly clamped or fully fastened, because mounting surfaces can pull a previously straight rail into a curve. If the indicator trace shows a repeating wave or a steady climb, you're not chasing a bad bearing—you're looking at the rail's true shape.
From Carport Canopies to Utility Arrays: Where These Channels End Up
These channels rarely stay in one place. A carport canopy might use a shorter run to bridge the gap between steel supports, holding panels just above a row of parked cars. The same profile, often with a mill finish or light anodizing, gets cut to length on site and secured with T-bolts that slide into the channel's grooves. Installers appreciate not having to drill extra holes—it's a matter of aligning the module clamps and torquing them down.
Move over to a utility-scale ground mount, and the channels multiply. Here they run in continuous rows, sometimes hundreds of meters long, anchored to driven piles or concrete ballast blocks. The loading changes: wind uplift, thermal expansion, and snow loads all push and pull on the channel. That's why the same extrusion gets a heavier wall or a different alloy, but the core function stays identical—giving modules a straight, reliable rail to sit on.
Between those two extremes you'll find rooftop commercial arrays, pergolas, and even solar awnings. The channel simply adapts to the span and the mounting surface. It's not glamorous, but it's the part that ties the whole system together, and most installations wouldn't stand for long without it.
After the Order Ships: Spare Parts, Retooling, and Real Support
A machine sitting idle costs more than its purchase price. That's why we keep a deep inventory of the parts that actually fail—bearings, seals, sensors—not just the ones that look good on a shelf. When a line goes down at 2 a.m., you don't need a callback in the morning; you need a courier with the right component in hand. Our warehouse team knows the difference.
Retooling isn't just for new products. Sometimes the fastest fix is sending a worn gearbox or pump back for a full rebuild—new bearings, reground shafts, fresh seals, all tested to original specs. It's often cheaper than buying new and gets you running in days, not weeks. We've seen too many shops scrap a perfectly good assembly because nobody offered them the option.
Real support means someone answers the phone who has actually touched the machine you're running. No scripted apologies, no ticket numbers that go nowhere. Just a direct line to an engineer who can walk you through a bypass, ship a part before you hang up, or flag a recurring failure so it doesn't bite you again next quarter.
FAQ
Start by asking for raw production footage instead of polished brochures. Factories that let you see their assembly floor and testing area on a video call tend to be more transparent. Also check how long they have been making solar-specific profiles, not just generic roll forming lines.
Pin down the exact profile drawings, material thickness range, punching patterns, and cutting tolerance. Ask whether the quoted price includes the decoiler, leveling unit, servo feeders, hydraulic punching, and flying saw. Many lower quotes later add these as extras.
Hebei, Jiangsu, and Shandong provinces have dense clusters of roll forming manufacturers. Within these, look for factories that specialize in solar mounting channels rather than general construction profiles, because the hole spacing and straightness requirements differ.
Request a live video tour of the workshop during assembly. Pay attention to the frame thickness, brand of PLC and motors, and whether they test-run the line with actual material before packing. Also ask for references from customers who bought solar channel machines specifically.
They often forget to specify hole pitch tolerances for mounting rails, or they assume all galvanized steel coils feed the same way. If you need punched holes on multiple faces, make sure the factory has experience with multi-axis punching units—not just a single-side press.
Expect 30 to 45 days for a standard solar channel roll forming line after drawings are approved. Shipping to major ports in North America, Europe, or Southeast Asia adds roughly 15 to 30 days depending on the route and customs clearance.
Ask for a detailed installation and operation manual with wiring diagrams, plus scheduled video support during commissioning. A factory that assigns a specific engineer to your project—rather than a general hotline—tends to resolve issues faster.
Conclusion
Step onto the floor of a top solar channel roll forming factory in China and you will see more than just machines cutting steel. Coils feed through stands at a steady pace, and each pass bends the metal a little closer to its final shape while operators check dimensions with calipers and feel the surface for inconsistencies. A custom profile drawing is not simply handed to a technician; it gets discussed at a workbench, marked up with notes on bend radii and flange heights, then translated into roll tooling that gets tested on a short run before full production starts. What surprises many first-time visitors is how much attention goes into coil thickness and coating. A galvanized layer that looks uniform on paper can behave differently under stress, so the best factories pull samples from every new coil and run a quick bend test to catch flaking or uneven zinc before it becomes a batch problem.
Beyond the visible forming work, straightness and tolerance checks happen at multiple stages. Rails that pass a casual glance can still warp once they leave the machine, so experienced operators use a granite table and a feeler gauge rather than relying on eyeballing alone. These channels end up in carport canopies, ground-mount arrays, and large utility projects where a few millimeters of twist creates installation headaches. That is why the strongest factories treat after-sales support as part of the manufacturing process, not an add-on. They keep spare roll sets on hand, offer retooling advice when a design changes, and answer phone calls about feed alignment or coating wear months after the order ships. A complete guide to these factories is not about listing equipment specs; it is about understanding the daily habits that separate reliable suppliers from those who only look good in a brochure.
Contact Us
Contact Person: Sophie
Email: [email protected]
Tel/WhatsApp: 8615959271231
Website: https://www.beenew-rollformer.com/